Answer Summary: Progressive die stamping is a high-volume metal forming process in which a continuous metal strip advances through multiple stations within a single die. Different stations can perform operations such as piercing, bending, and forming before the finished part is separated from the carrier strip. For suitable OEM parts and production volumes, progressive tooling can combine multiple operations into a repeatable automated production process.
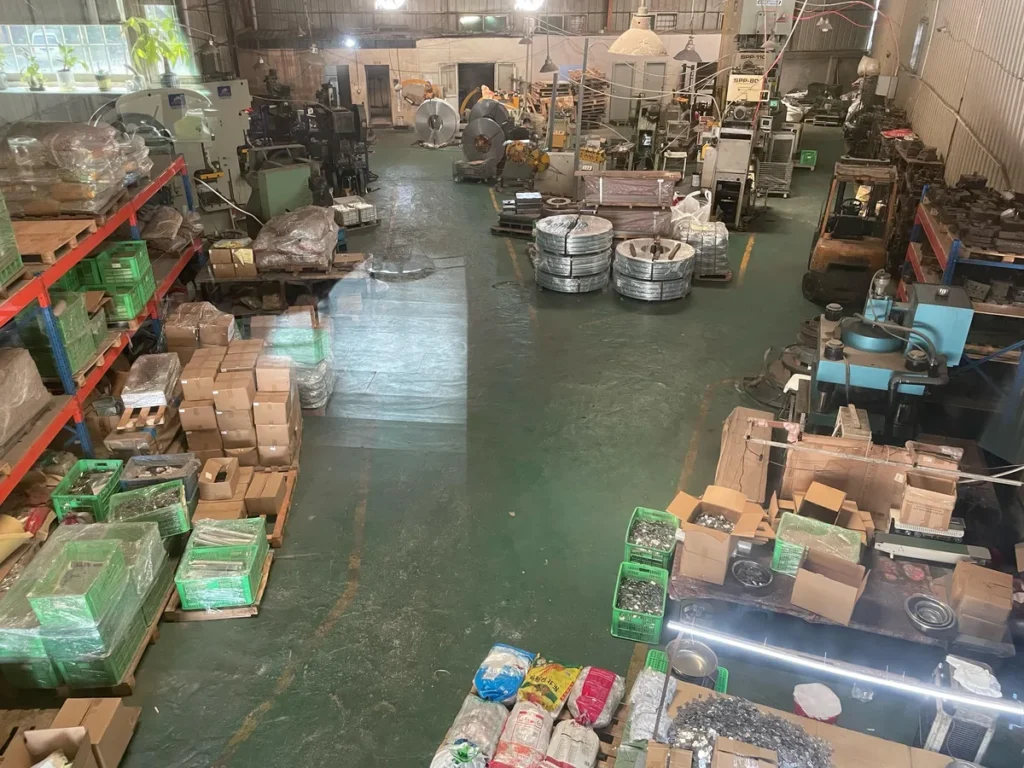
Metal Stamp Factory designs and builds progressive dies in-house at our facility in Xiamen, China. Our founder, Shengtong Chen, has more than 25 years of hands-on experience in tooling development and metal stamping. If you’re new to metal stamping in general, start with our guide on metal stamping first.
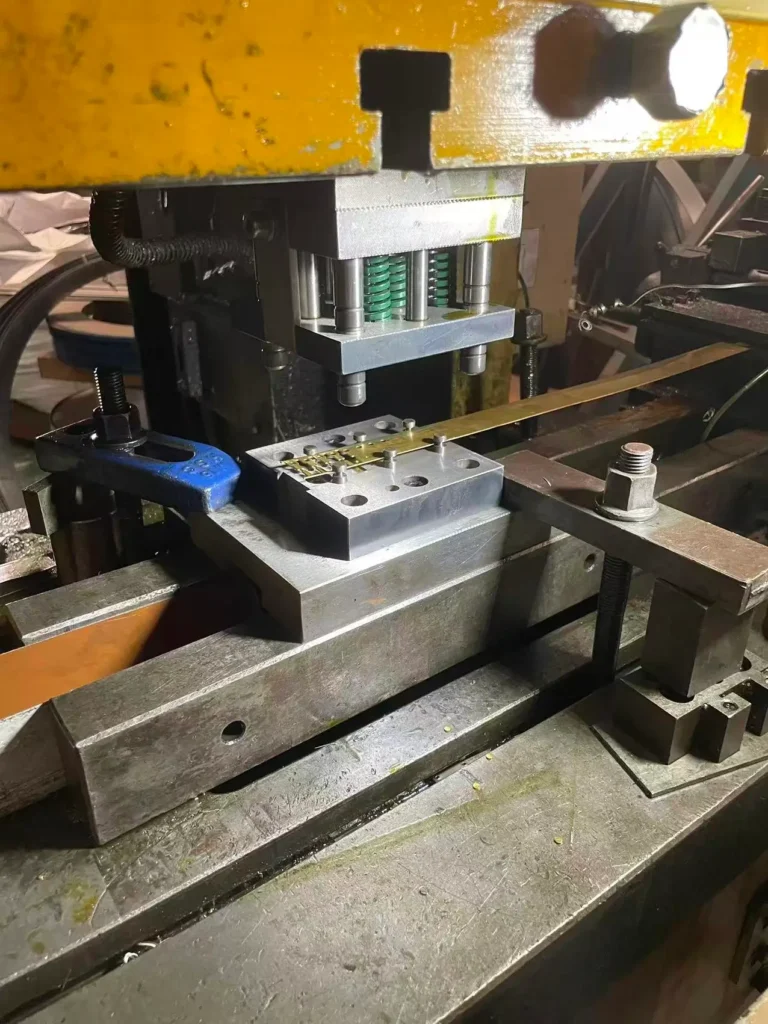
What Is Progressive Die Stamping?
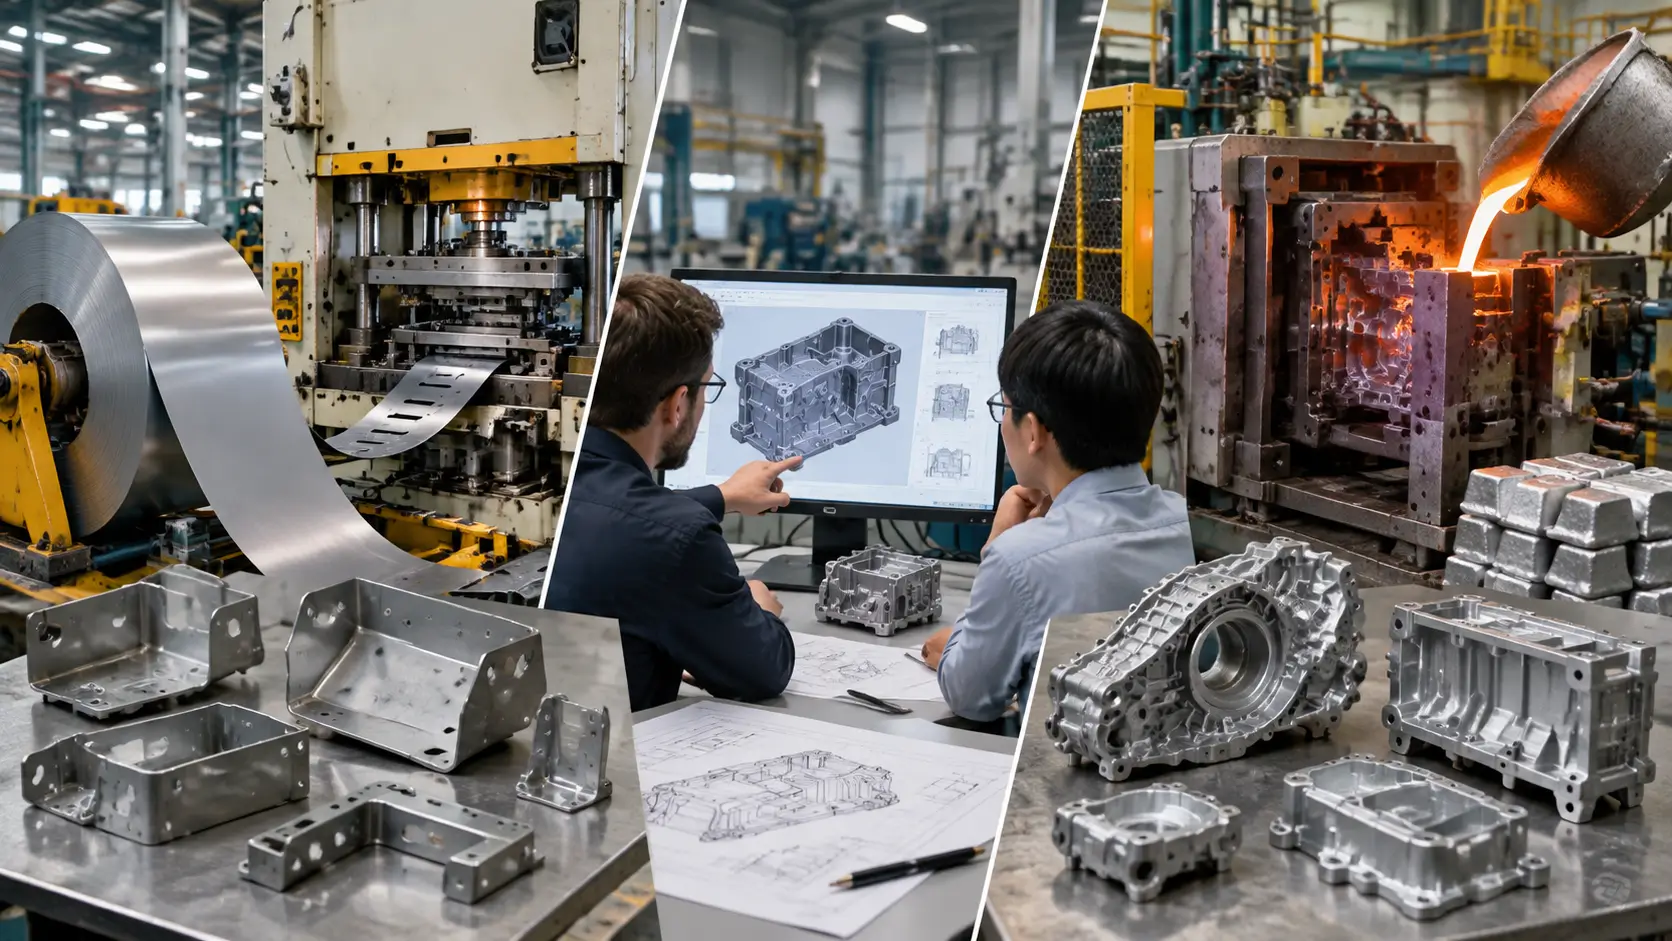
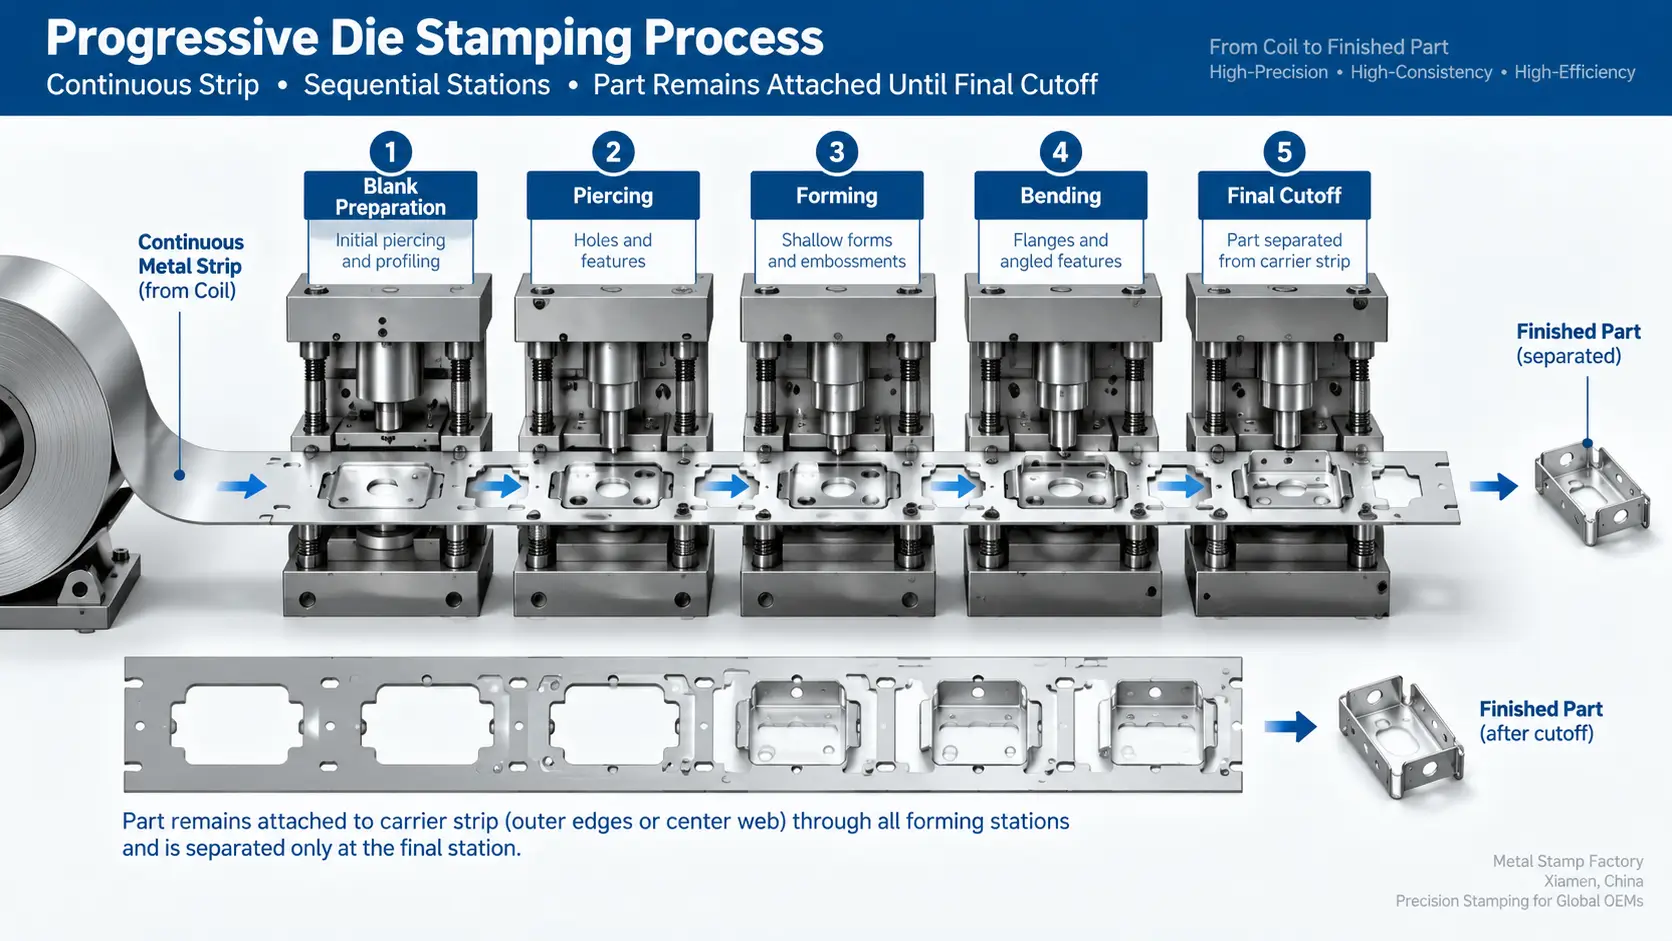
Progressive die stamping is a metal forming process that uses a single die with multiple stations arranged in sequence. A coil of metal strip feeds through the press, and at each station a different operation is performed — piercing, bending, coining, or forming — until the part is fully formed by the time it exits the final station.
Unlike single-station stamping, where separate operations may require additional handling or repositioning, progressive die stamping keeps the strip connected to a carrier as it advances through the die. Each press stroke advances the strip by a defined feed pitch, allowing multiple stations to work on different portions of the strip at the same time. Depending on the die layout, finished parts can be separated at the final station as production continues.
How Does a Progressive Die Work?
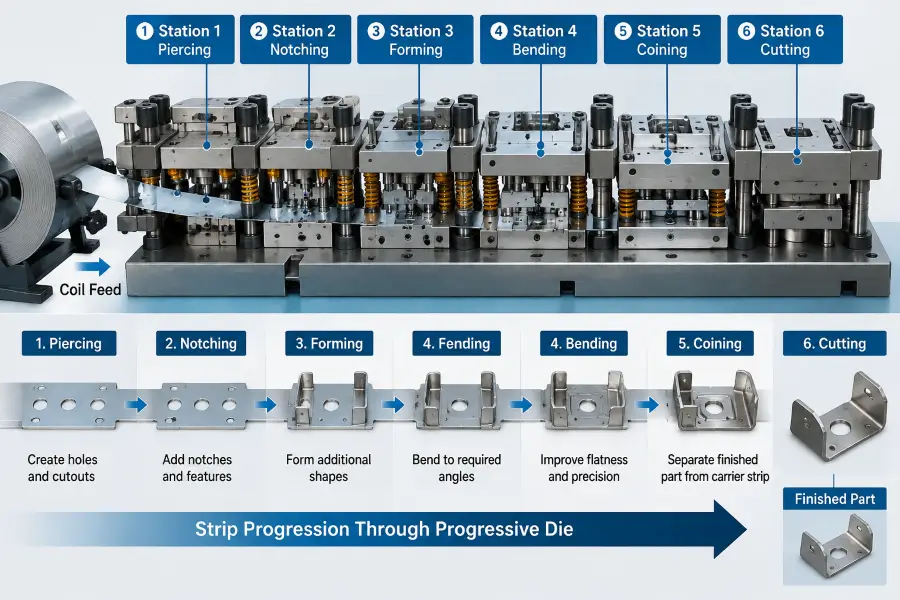
The progressive stamping process moves through a fixed sequence within a single die:
Progressive Die Stamping Process Flow
| Stage | Operation | Purpose |
|---|---|---|
| Material Feeding | Coil strip feeding into the die | Ensures continuous and accurate material positioning |
| Piercing | Creating holes and internal features | Produces required openings and cut features |
| Bending | Forming angles and shapes | Creates required part geometry |
| Forming | Creating three-dimensional features | Produces complex stamped shapes |
| Cutting | Separating finished parts | Releases completed components from the strip |
| Final Inspection | Checking dimensions and quality | Confirms parts meet OEM requirements |
Step 1 — Material Feeding: Coil stock feeds into the press and advances a set distance with each stroke.
Step 2 — Piercing: Holes and cutouts are punched into the strip at early stations.
Step 3 — Bending: The strip is bent into shape at designated stations.
Step 4 — Forming: Additional forming operations shape features that piercing and bending alone can’t produce.
Step 5 — Cutting: The finished part is separated (blanked) from the carrier strip.
Step 6 — Finished Part: The completed part is separated from the carrier strip at the final stage of the die sequence.
Main Components of a Progressive Die
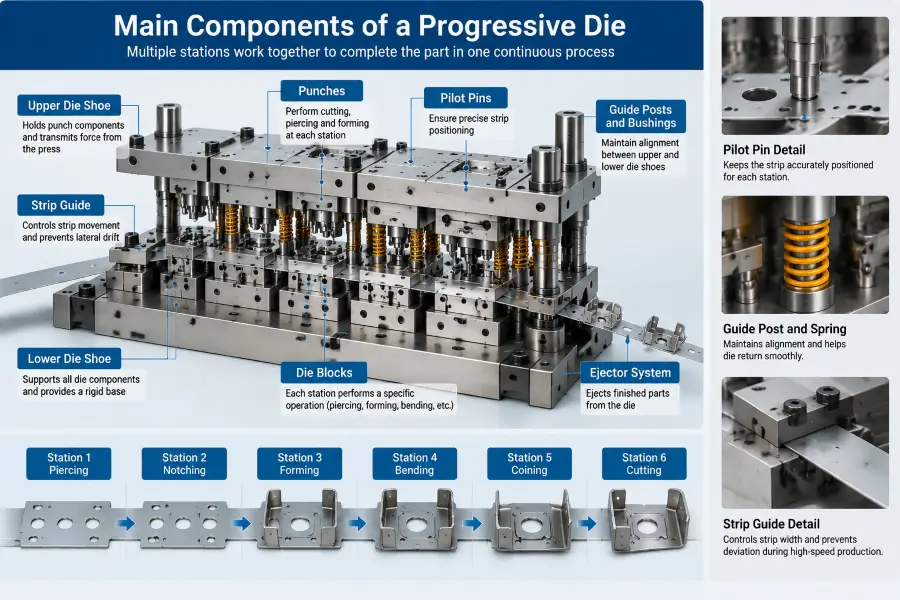
A progressive die is built from several precision components working together:
Die plate — the base structure holding all tooling components in alignment
Punches and dies — the cutting and forming tools at each station
Guide pins and pilot pins — keep the strip precisely positioned as it advances
Strip guide — controls strip movement and prevents lateral drift
Sensors (where applicable) — detect misfeeds or strip breakage to stop the press before damage occurs
Progressive Die Stamping Process Step by Step
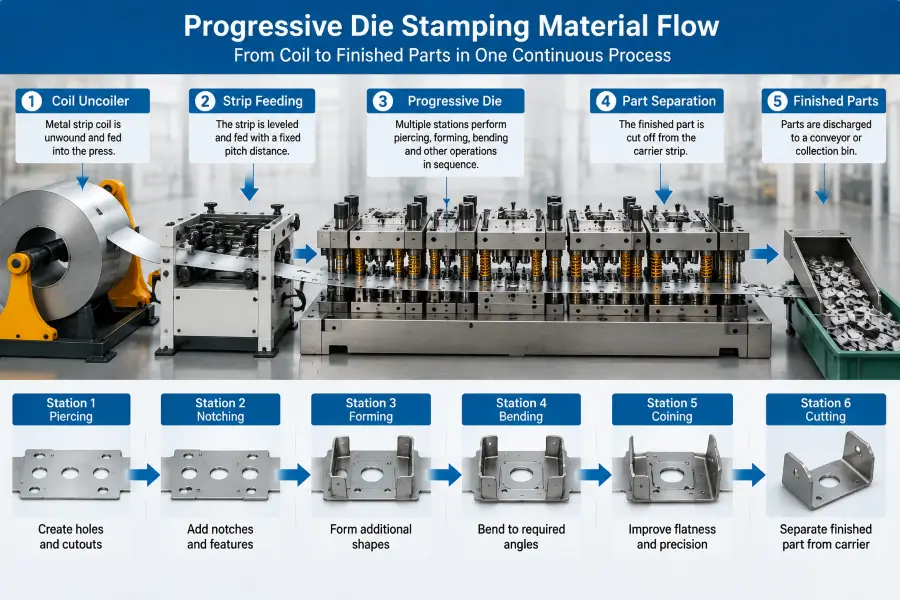
This is a simplified, progressive-die-specific view of the process — for the complete production process from drawing to delivery, see our metal stamping process guide.
For a custom OEM project, the full process runs through these stages:
Step 1 — Engineering Drawing Review The customer’s drawing is reviewed for material thickness, part geometry, tolerances, and production volume before quoting tooling.
Step 2 — Material Selection The right material grade and thickness are confirmed based on the part’s strength, corrosion resistance, and forming requirements.
Step 3 — Progressive Die Design Engineers design the die layout — how many stations, what each station does, and the sequence of operations.
Step 4 — Tool Manufacturing The progressive die is built and assembled in-house.
Step 5 — Trial Stamping The new die runs a trial batch to check forming accuracy and part consistency.
Step 6 — Sample Inspection Trial parts are checked against the drawing and sent for customer approval before mass production.
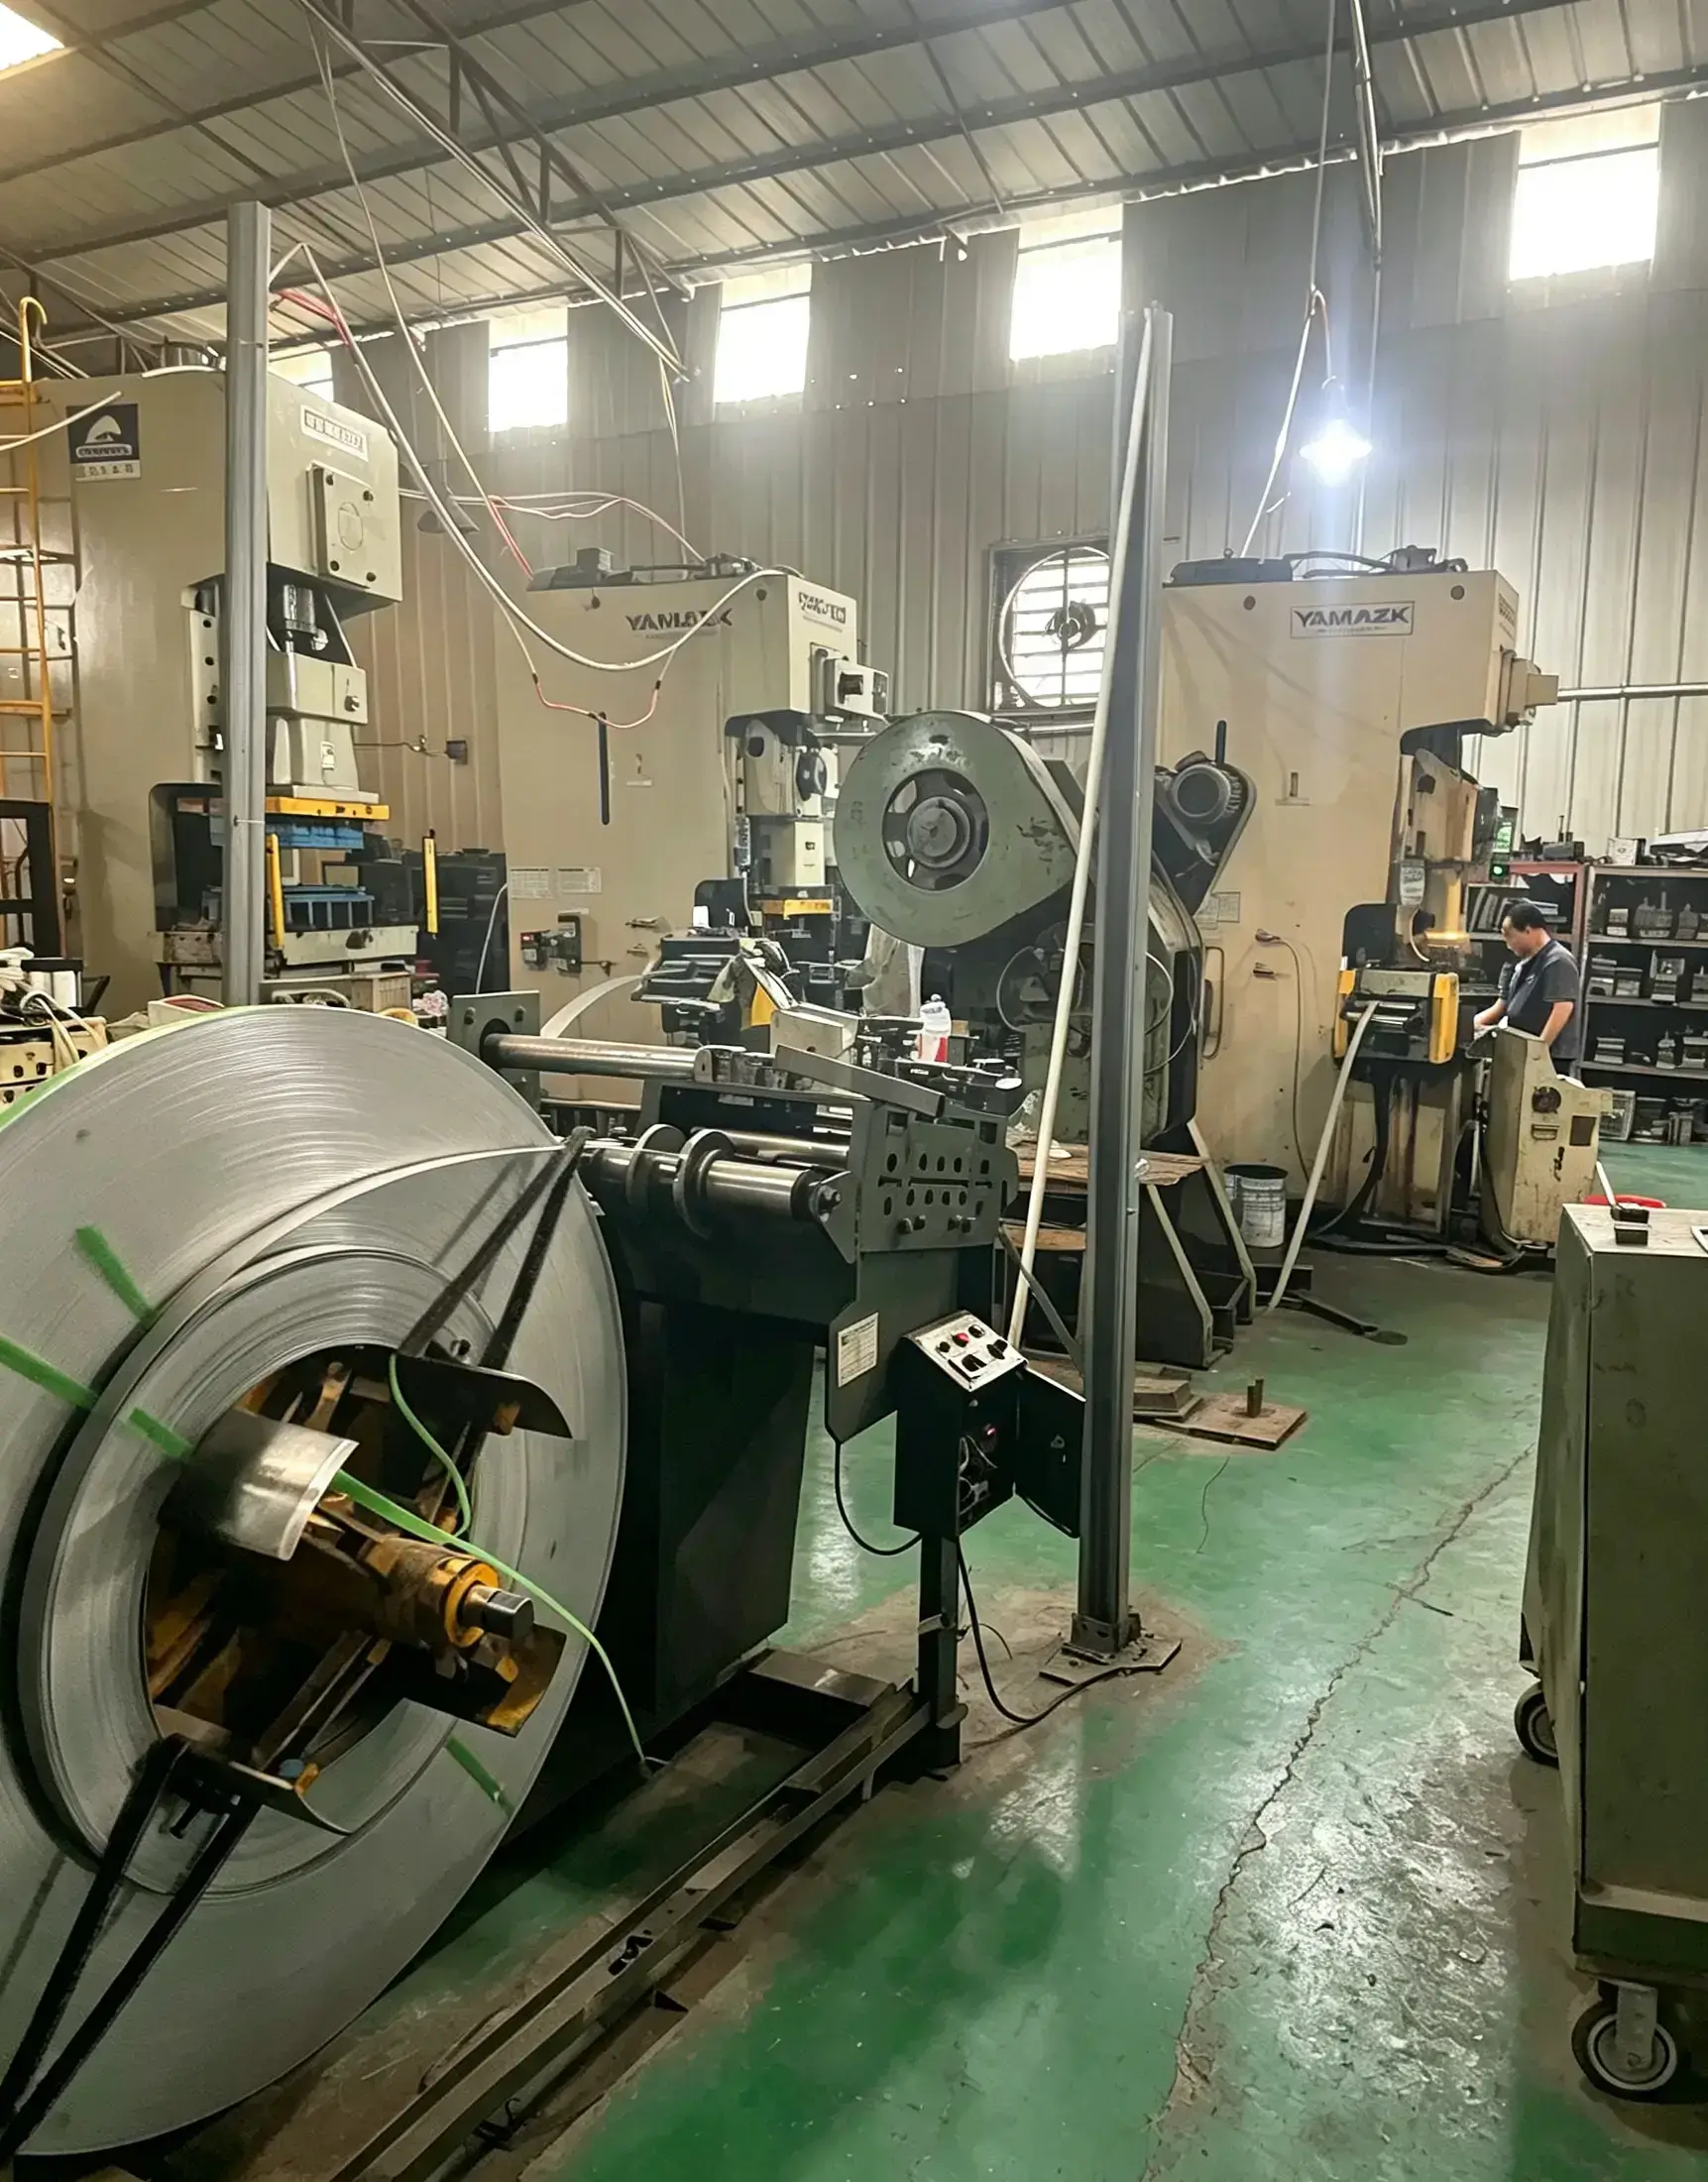
Step 7 — Mass Production Once samples are approved, the die runs continuously with automatic coil feeding for high-speed output.
Step 8 — Quality Inspection Finished parts are checked throughout the run and before shipment.
From the factory floor: At Metal Stamp Factory, progressive die projects usually start with drawing review before tooling quotation. Our engineering team evaluates material properties, part geometry, tolerances, and production volume to confirm whether a progressive die is the right approach for a given part. For detailed information about stamping tolerance requirements and quality standards, see our guide on metal stamping tolerances.
For complex parts with multiple features, die design has to balance forming sequence, material flow, and tool durability — a poorly sequenced station order can cause deformation, excessive scrap, or unstable production down the line.
What Materials Can Be Used for Progressive Die Stamping?
Progressive die stamping works with a wide range of metals:
1. Stainless steel (304, 316)
2. Carbon steel
3. Galvanized steel
4. Aluminum
5. Copper and brass
Material choice affects forming behavior, spring-back, and die wear — see our full metal stamping materials guide for properties and typical uses. Material specifications may also reference standards published by ASTM International.
Progressive Die Stamping Applications
Progressive die stamping is used across a wide range of industries:
Automotive & Motorcycle — brackets, reinforcement components, connector parts, and other stamped hardware where the part geometry and production requirements are suitable for progressive tooling.
Solar / Photovoltaic — end clamps, mid clamps, rail splices, grounding clips, and mounting brackets
Electronics and Electrical — terminal strips, contact springs, EMI shielding components
Industrial Equipment — hinges, brackets, fastener components
For terminal and connector components, progressive tooling can integrate operations such as piercing, bending, and forming across sequential stations. Surface finishing such as plating, when required by the project, is typically performed as a separate operation after stamping. In our actual electrical component production, we manufacture copper terminal components by progressive die stamping followed by tin plating, and phosphor bronze spring contacts for power-strip applications using progressive die tooling.
You can browse more examples on our case studies page.
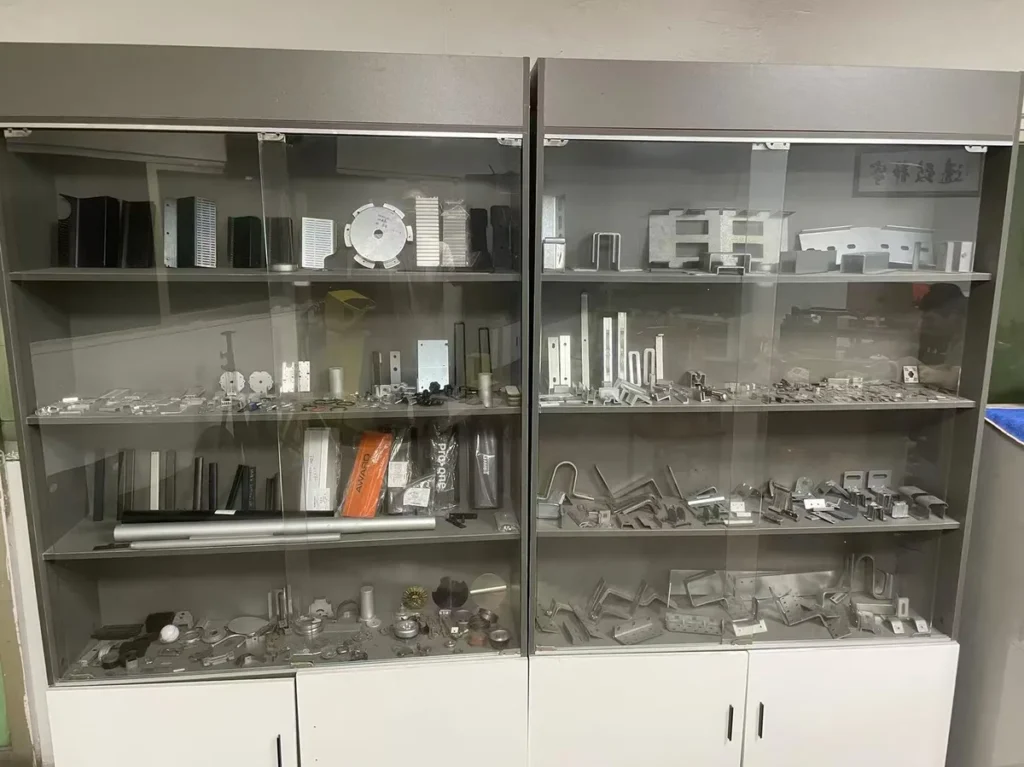
Progressive Die Stamping Advantages
| Advantage | Why It Matters |
|---|---|
| High production speed | Multiple stations operate simultaneously as the strip advances through the die |
| Lower per-unit labor cost | Minimal manual handling once tooling is set up |
| Stable, consistent quality | Every part is formed within the same die set |
| Suitable for high volume | Tooling cost is spread across a large unit count |
Limitations of Progressive Die Stamping
Higher initial tooling investment — progressive dies combine multiple stations in one tool, so the upfront tooling investment must be evaluated against the expected production requirements.
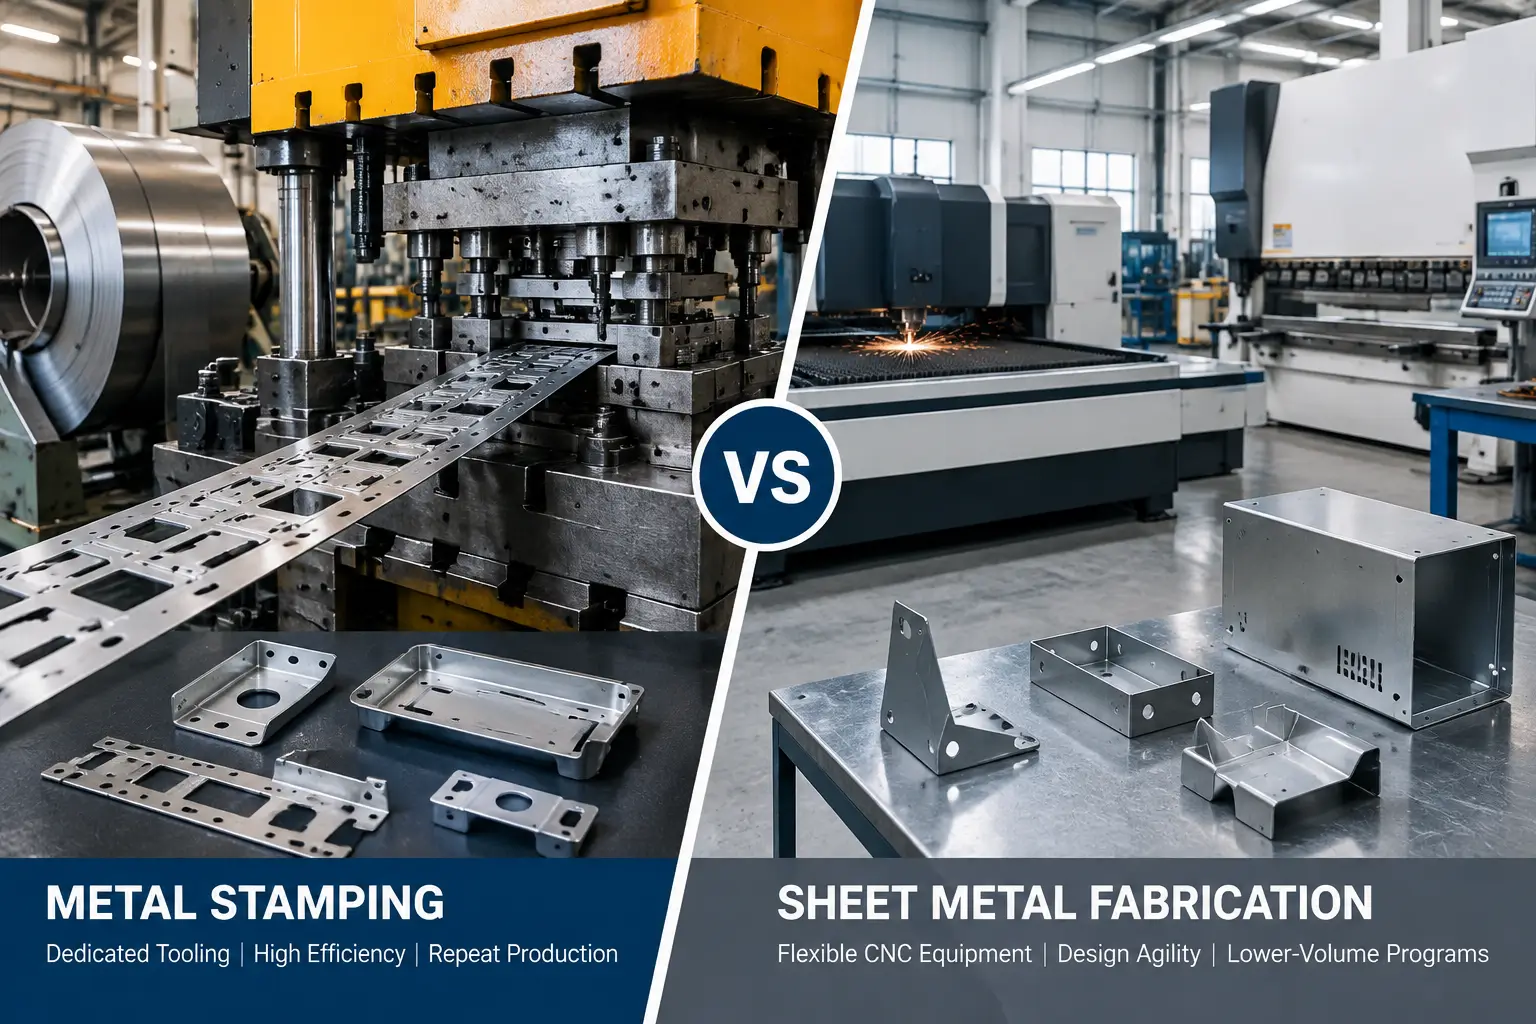
Less suitable for prototypes or very low volumes — when production quantity is limited, a simpler tooling or fabrication approach may be more economical depending on the part.
Complex parts require engineering evaluation — some geometries need a different process (transfer die, deep draw) instead
Progressive Die Stamping vs Transfer Stamping
| Comparison | Progressive Die | Transfer Die |
|---|---|---|
| Part handling | Strip-connected throughout the process | Parts transferred individually between stations |
| Best suited for | Strip-fed parts suited to sequential operations | Parts better handled as individual blanks between stations |
| Production rate | Can support high production rates | Depends on part geometry and the transfer system |
| Forming approach | Multiple operations performed while the part remains connected to the carrier strip | Individual parts move between separate forming stations |
Transfer die stamping can be suitable for parts that are better handled as individual blanks between stations, while progressive die stamping is commonly used for strip-fed parts that can be formed through sequential operations. The appropriate process depends on part geometry, material behavior, forming requirements, production volume, and tooling strategy.
Progressive Die Stamping vs Deep Draw Stamping
Progressive die stamping forms features across sequential stations while the material remains connected to a strip carrier. Deep drawing uses a punch and die to draw sheet metal into a cavity to create cup-like, box-like, or other drawn shapes. Which process is more suitable depends on the part geometry, draw requirements, material behavior, production volume, and tooling strategy.
Progressive Die Stamping vs Four Slide Stamping
Four-slide or multi-slide forming uses multiple slides acting from different directions and is commonly applied to small strip or wire-formed parts with several bends. Progressive die stamping advances strip stock through sequential in-line stations. The appropriate process depends on part geometry, material, forming direction, production volume, and available equipment.
Fine blanking is a specialized process used when a project requires controlled cut-edge quality and tight dimensional requirements. It uses dedicated tooling and equipment that differ from conventional stamping. For conventional progressive-die projects, edge condition depends on factors such as die clearance, tool condition, material, and cutting geometry, so burr and edge requirements should be defined on the drawing and evaluated during tooling review. Edge quality is also an important consideration for stamped products such as our stainless steel bird spikes, where the stamped base plate is produced using progressive die tooling.
Progressive Die Stamping vs Traditional Press Stamping
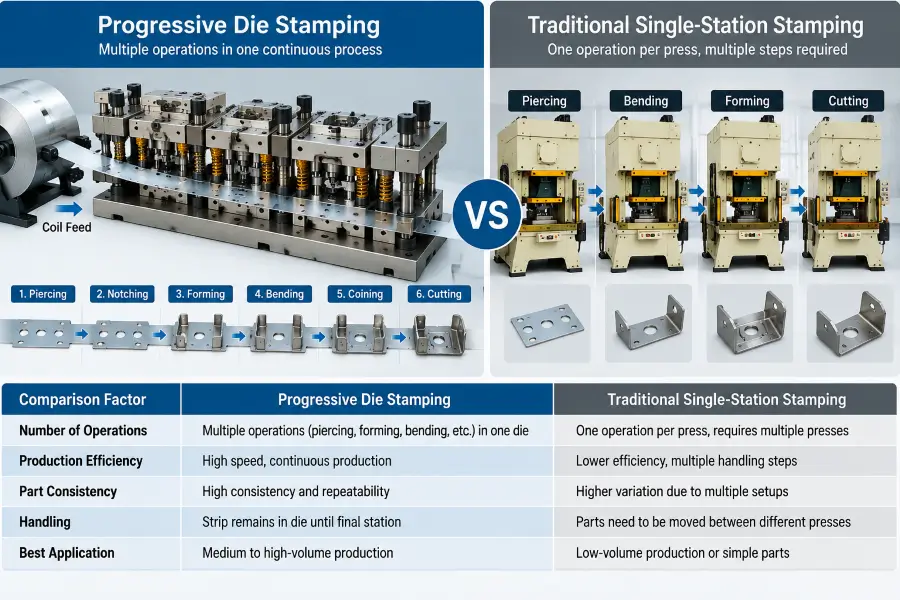
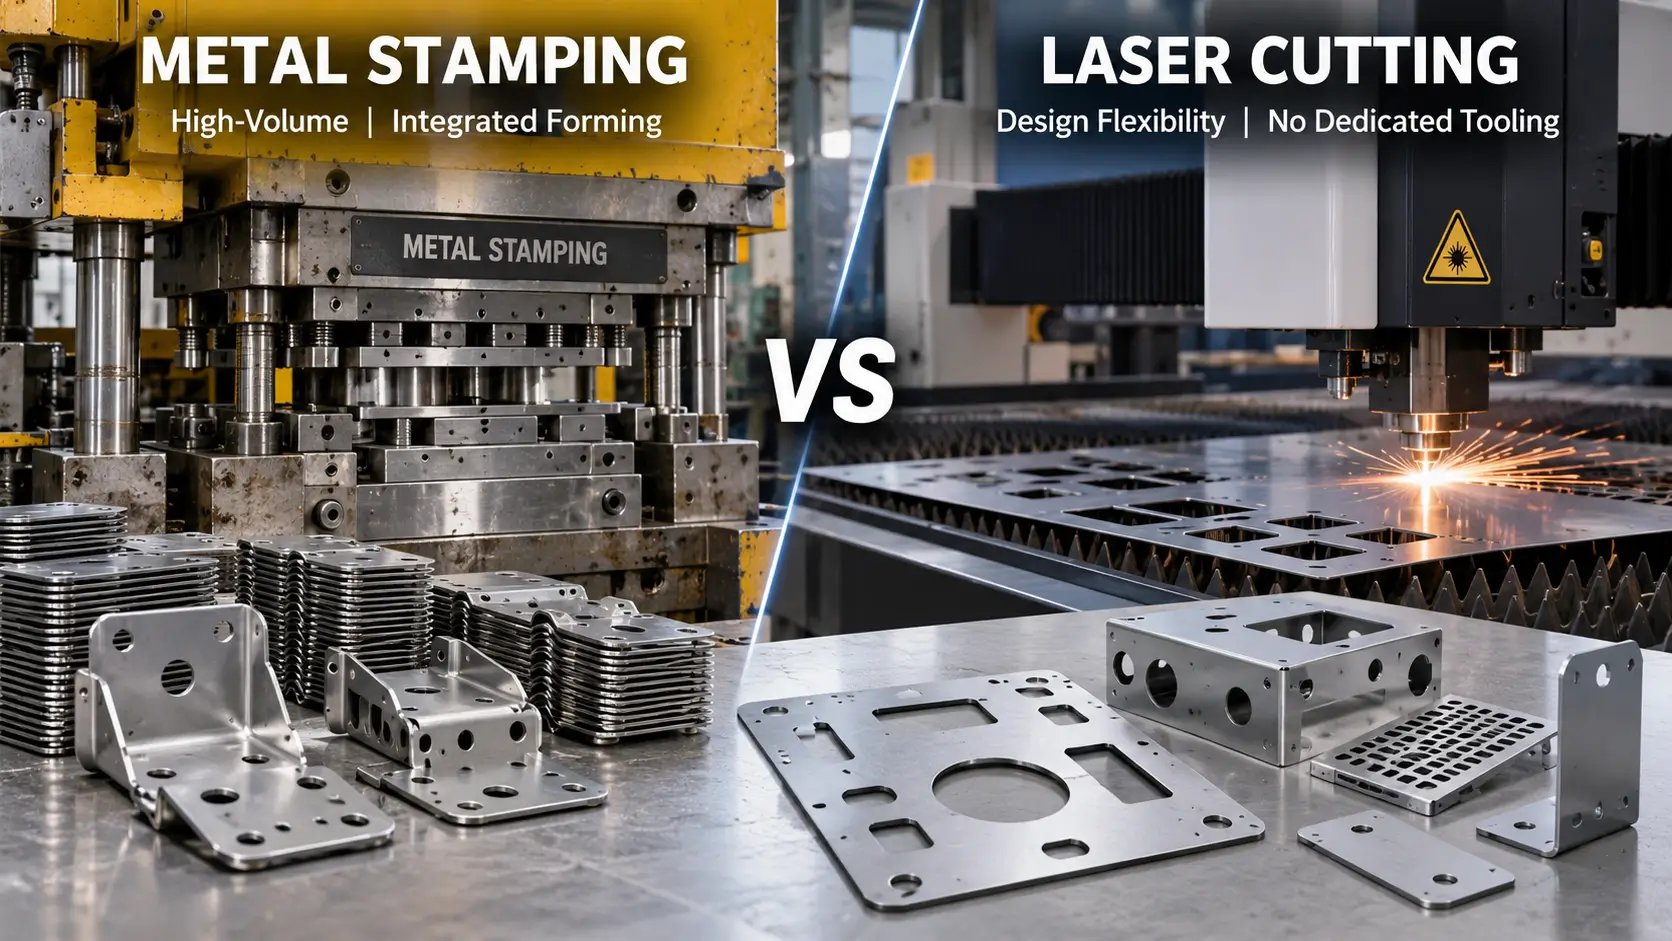
Single-station stamping performs one primary operation at a time and may require additional handling between operations. Progressive die stamping integrates multiple operations across sequential stations in one die. Which approach is more economical depends on part geometry, tooling requirements, production quantity, and expected repeat demand.
When Should You Choose Progressive Die Stamping?
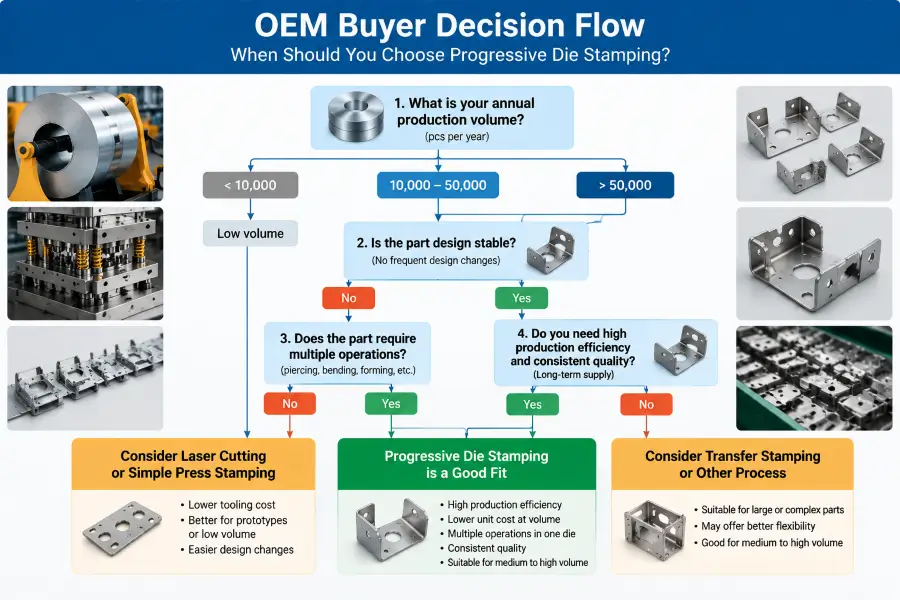
Progressive die stamping is a strong fit when:
Progressive Die Stamping Suitability Checklist
| Requirement | Progressive Die Suitability |
|---|---|
| Annual production volume | Best for medium to high-volume production |
| Part design stability | Recommended when design changes are limited |
| Multiple stamping operations | Excellent for combining several operations |
| Tight repeatability requirements | Suitable for consistent mass production |
| Prototype production | Usually not the first choice |
| Frequent design changes | Less suitable due to tooling modification cost |
✔ You need high production volume
✔ The part design is stable and unlikely to change frequently
✔ The part requires multiple operations (piercing, bending, forming) in sequence
When Progressive Die Stamping Is Not the Best Choice
Progressive die stamping is usually not the right fit for:
✘ Prototypes or one-off parts
✘ Very small production quantities
✘ Very large parts that don’t suit strip-fed tooling
For these cases, a simple single-station die, transfer stamping, or another process is often a better starting point — talk to us about your part and we’ll recommend the right approach.
How Much Does Progressive Die Stamping Cost?
| Cost Factor | Impact |
|---|---|
| Die design and tooling | Largest upfront cost; complexity and number of stations drive it up |
| Material | Grade, thickness, and coating affect raw material cost |
| Part complexity | More stations and tighter tolerances increase tooling cost |
| Production volume | Higher volume lowers per-part cost |
| Secondary operations | Plating, coating, or assembly add per-part cost |
How Long Does Progressive Die Tooling Take?
For many custom projects, progressive die tooling usually requires around 35–40 days after tooling approval, depending on part complexity and die structure. A simpler single-station die typically takes less time — around 15–25 days — since it involves fewer stations and less die-flow engineering.
How to Choose a Progressive Die Stamping Manufacturer?
Progressive Die Stamping Supplier Evaluation Checklist
| Evaluation Factor | What OEM Buyers Should Check |
|---|---|
| Tooling Capability | In-house die design and manufacturing experience |
| Press Capacity | Available tonnage, automation, and production capability |
| Engineering Support | DFM review and process optimization capability |
| Quality Control | Inspection equipment and quality management process |
| Manufacturing Experience | Similar stamped parts and industry experience |
When evaluating a progressive die stamping supplier, look at:
In-house tooling capability — a supplier that designs, builds, and maintains its own dies can provide more direct control over tooling development, modification, and maintenance.
Press capacity and equipment fit — confirm that the available presses, feeding equipment, and tooling capability are appropriate for the material, part geometry, and required operations.
Quality inspection process — ask specifically what gets checked, not just whether they have a “quality system”
Experience with your part type — ask for relevant case studies or sample parts, not just a general capability list
We cover this in full detail in our companion guide: Buyer Guide: How to Choose a Metal Stamping Manufacturer.
If your project needs more than progressive die work, see our full custom metal stamping services for everything we handle in-house.
Quality Control in Progressive Die Stamping Production
Our process includes:
Incoming material inspection — confirming grade, thickness, and coating against the mill test certificate
First article inspection — checking the first parts off the die against the drawing before production continues
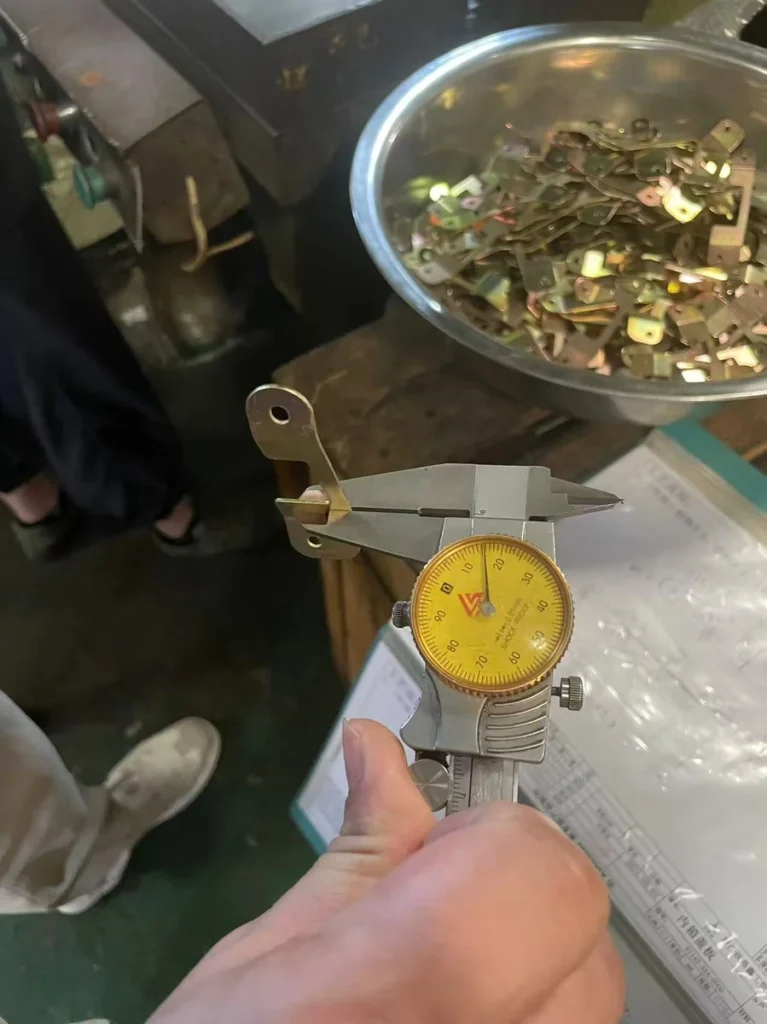
Dimensional inspection — periodic sampling during the run using calipers to catch tool wear early
Production monitoring — ongoing checks throughout the run, not just at the start and end
Progressive Die Stamping FAQ
What is progressive die stamping used for? It’s used to produce small to medium metal parts at high volume with multiple features — brackets, clips, terminals, connectors, and similar components — across automotive, solar, electronics, and industrial applications.
Is progressive stamping cheaper than traditional stamping? At high volume, yes — tooling cost is spread across a large number of parts, driving down per-unit cost. At low volume, the higher upfront tooling investment usually makes a simpler single-station die more economical.
How long does a progressive die last? Die life depends on material, part complexity, and production volume — regular maintenance and monitoring for wear extends usable die life significantly.
What materials can be stamped? Common materials include stainless steel, carbon steel, galvanized steel, aluminum, copper, and brass — material choice depends on strength, corrosion resistance, and formability requirements.
What is the minimum order quantity? MOQ depends on part complexity and tooling investment — progressive die stamping becomes most cost-effective at higher volumes where tooling cost amortizes across more parts. Tell us your part and target volume and we’ll quote honestly based on what it actually takes.
Conclusion: Is Progressive Die Stamping Right for Your Project?
Metal Stamp Factory was established in 2014 in Xiamen, China, focusing on custom metal stamping and precision hardware manufacturing. The founder of Metal Stamp Factory, Shengtong Chen, started learning mold making and metal stamping at the age of 17 and has accumulated more than 25 years of hands-on manufacturing experience in tooling development, metal stamping, and OEM production.
If your part needs high-volume production with multiple forming operations and a stable design, progressive die stamping is likely the right fit. If you’re still deciding, send us your drawing and target quantity — our engineering team will review the project and recommend the right tooling approach.